Select Country or Region

global

English

Blog Center

Blog Details

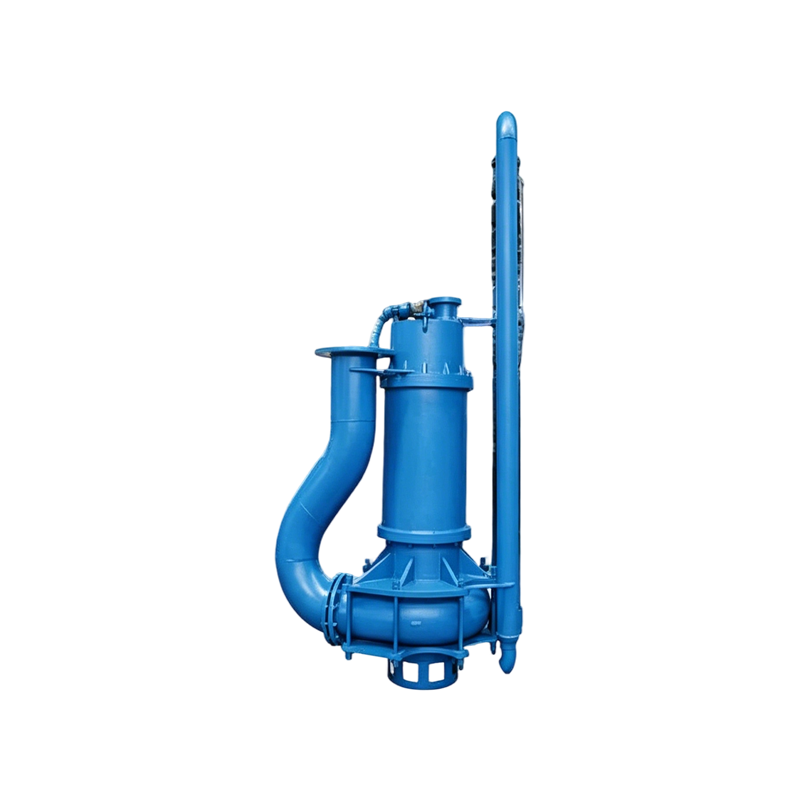
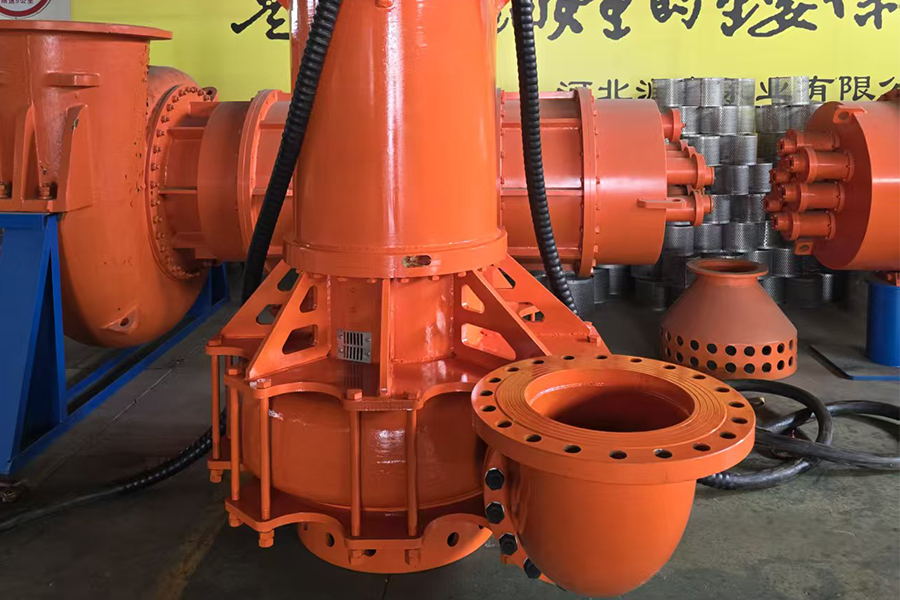
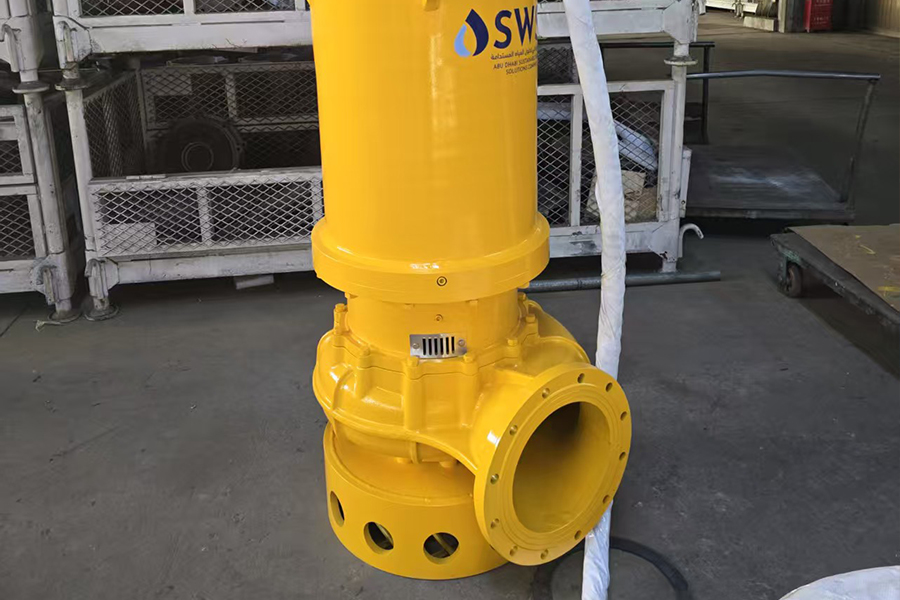
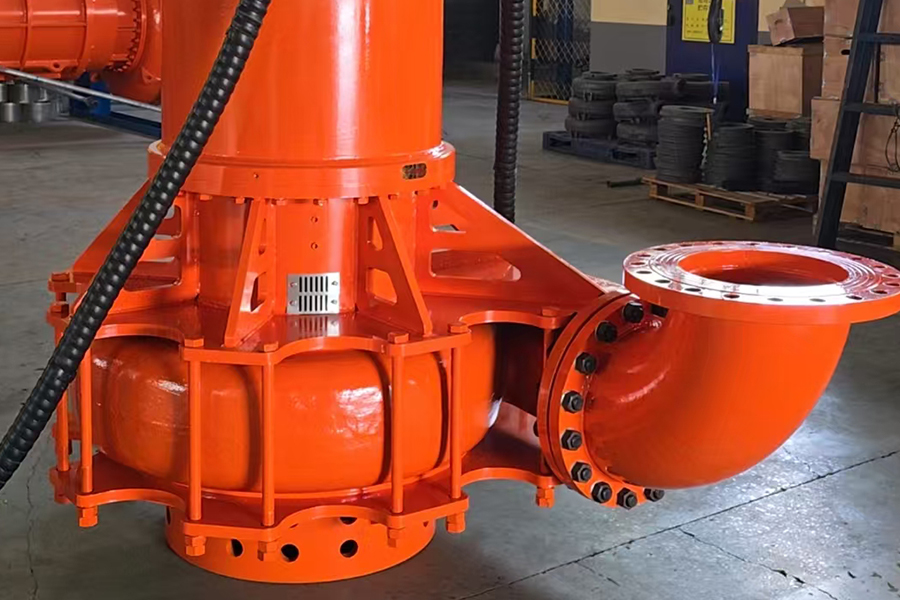
What Needs to Be Confirmed for the Selection of Explosion-Proof Submersible Slurry Pumps?

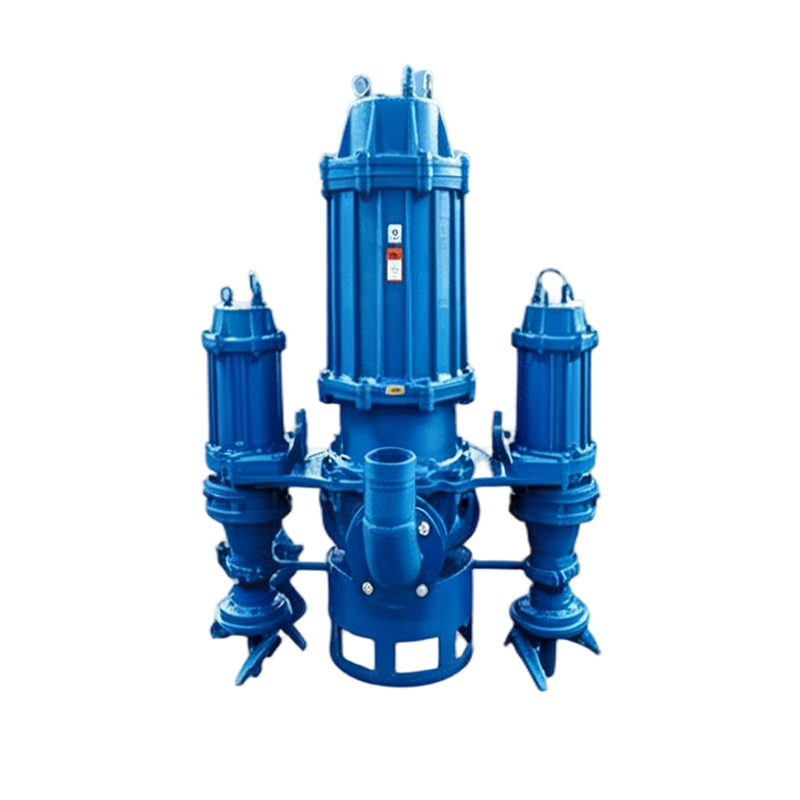
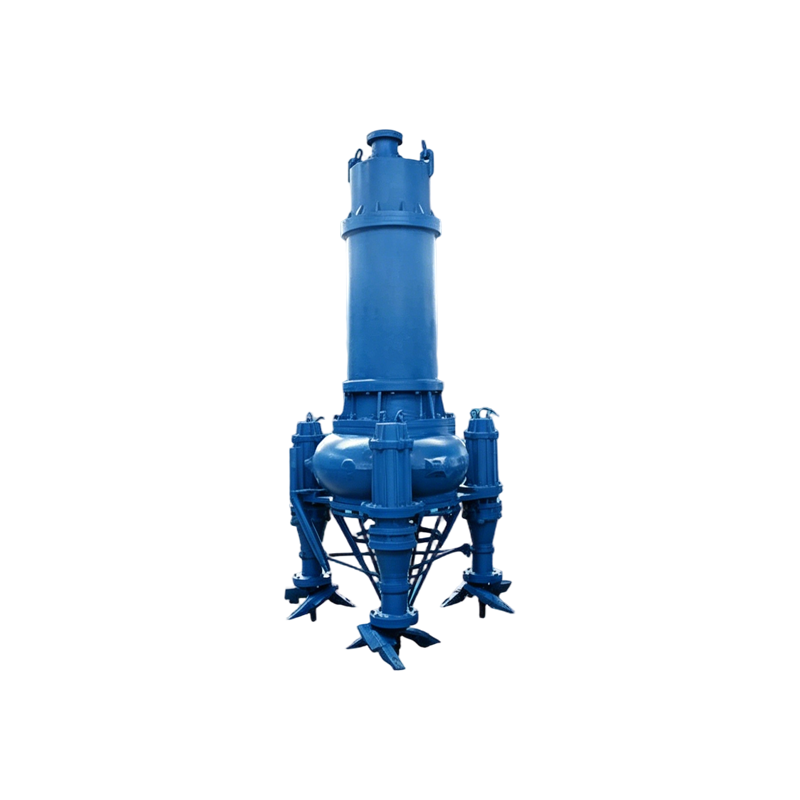
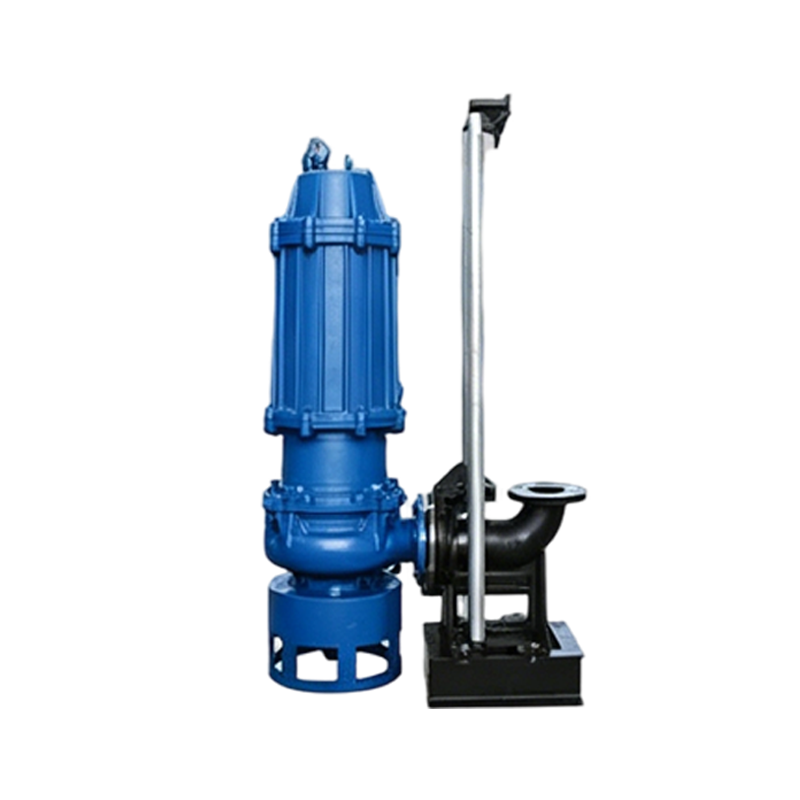
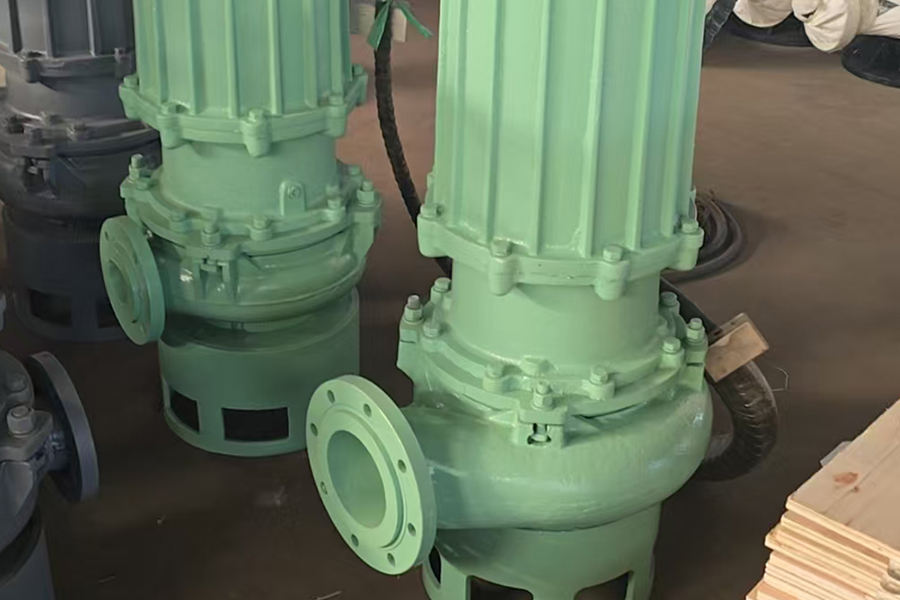
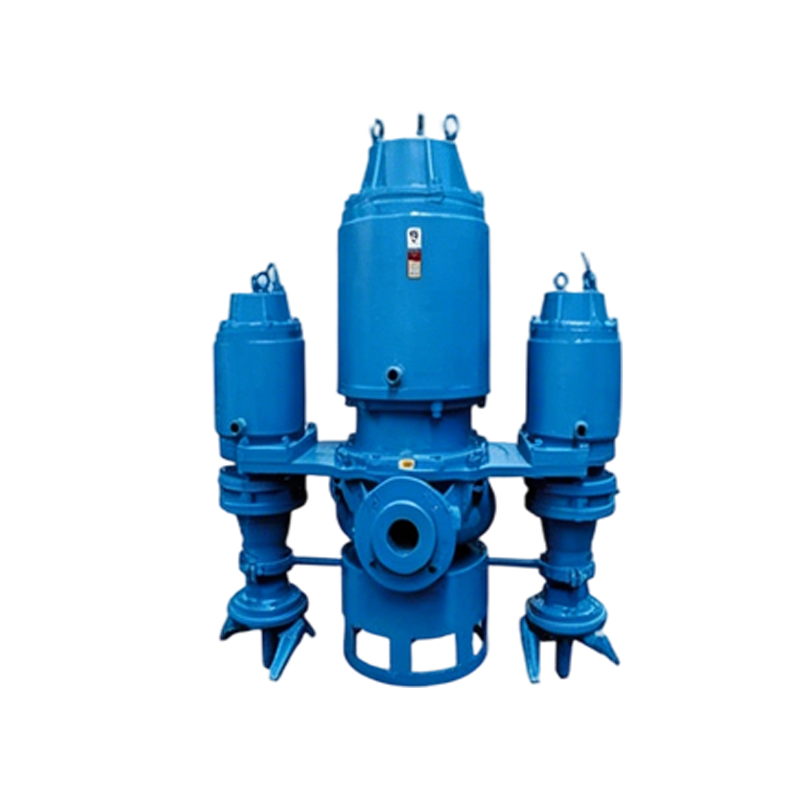
Explosion-proof submersible slurry pumps are used for slurry transport environments where there may be risks of flammable gases, vapors, or dust. They must not only meet flow rate, head, and wear resistance requirements, but also comply with safety regulations for hazardous areas on site.

Before selection, the following need to be confirmed:

1. Hazardous area classification;

2. Name of flammable gas or dust;

3. Explosion-proof rating;

4. Temperature class;

5. Standards adopted by the project;

6. Destination country and certification requirements;

7. Voltage, frequency, and control method.

At the same time, basic operating conditions of the pump must be provided, including flow rate, head, medium, solid content, particle size, temperature, corrosiveness, submersion depth, and pipeline conditions.

Standard submersible slurry pumps cannot be directly used in explosion-proof areas without confirmation. The installation, wiring, and maintenance of explosion-proof pumps must also not alter the flameproof structure or bypass protective devices without authorization.

When requesting a quote, both operating conditions and explosion-proof requirements should be submitted simultaneously, so that technical personnel can confirm the product structure, applicable rating, and available certification documents.

Company FAQs
FAQ
Here, we answer your frequently asked questions about customization, material selection, and purchasing industrial rubber and wear-resistant components.
Contact Us
What parameters are needed to quote a submersible slurry pump?
Please specify flow rate, head, slurry type, solid content, max particle size, slurry density, submersion depth, operating hours, mounting method, voltage/frequency, and operating environment.
Can submersible slurry pumps handle large particles or high-density slurries?
Select models can be configured for large solids, high concentrations, or abrasive slurries. Actual capacities depend on pump model, impeller design, wet-end materials, and operating conditions.
What are the differences between submersible slurry pump types?
Designed for specific operating conditions: Agitator type: For sediments and high-density slurries; High-flow type: For large delivery capacities; Explosion-proof type: For hazardous or explosive areas; High-pressure jetting type: For flushing, loosening, or desilting; Coupled type: For specific drives and mounting setups; Forced-cooling type: For continuous duty or high heat dissipation needs.
How to select the right submersible slurry pump?
Selection depends on flow rate, head, slurry concentration, particle size, medium density, suction conditions, submersion depth, operating hours, and on-site mounting.
What applications are slurry pump series suitable for?
Slurry pumps mainly transport solid-laden slurries, mud, mortar, tailings, and sediments, ideal for mining, mineral processing, dredging, gravel handling, and industrial slag disposal.

Ready to upgrade your
pumping system?

Global Inquiry Hotline

+86 19933037056

Official Email

info@cnminerals.com

Company Address

Block C, MCC Shengshi Plaza, No. 66 Xiangtai Road, Yuhua District, Shijiazhuang City, Hebei Province

Get Free Custom Solution

*
*
File Upload Upload your drawings for a real-time quote